

Why Modern Manufacturing Runs On ERP Systems
Picture a busy manufacturing plant trying to function without a central nervous system. The purchasing team orders raw materials using inventory sheets from last week. The production line is working off a schedule that doesn’t know a key machine just went down. Over in the finance department, they’re pulling their hair out trying to calculate the true cost of a finished product because the data lives in a dozen different spreadsheets. This kind of chaos is exactly what a manufacturing ERP is built to prevent.
An Enterprise Resource Planning (ERP) system is, in essence, the digital brain of your entire operation. It doesn’t just hold onto information; it weaves it all together in real time. It’s like the ultimate project manager—one that sees everything happening at once and makes sure every department is reading from the same script.
A Unified View for a Complex Environment
Manufacturing is a complicated dance with countless moving parts. A single delay in a shipment of raw materials can bring a whole production line to a grinding halt, costing thousands in lost time and productivity. An ERP system is your best defence against these expensive information gaps.
For instance, when a salesperson lands a big new order and enters it into the system, the ERP immediately checks your stock levels. If you’re running low on a critical component, it automatically flags it for the procurement team to reorder. At the same time, it slots the new job into the production schedule, making sure the shop floor has the capacity to get it done without throwing existing work into disarray.
A well-implemented ERP system is the difference between constantly fighting fires and having true operational control. It gives you the foresight to manage resources well, spot bottlenecks before they happen, and pivot quickly when demand or supply changes.
This seamless connectivity is what makes an ERP non-negotiable today. It breaks down the walls between departments and gets you away from fragmented data living in silos. The result is a unified, cohesive operation. This single source of truth gives everyone, from the machine operator to the CEO, the accurate, up-to-the-minute information they need to make better decisions and stay competitive.
Ultimately, a manufacturing ERP delivers:
- Real-time Visibility: See exactly what you have in stock, the status of every job, and where your shipments are at any given moment.
- Improved Collaboration: Keep your finance, purchasing, and production teams perfectly in sync.
- Data-Driven Decisions: Swap guesswork for accurate analytics when you’re forecasting and planning.
- Enhanced Efficiency: Automate repetitive tasks and fine-tune your workflows to cut down on waste and delays.
The Real-World Benefits of a Manufacturing ERP
Let’s move past the theory. What does a manufacturing ERP actually do for your business? Putting this kind of system in place is a big step, but the rewards are real and measurable, showing up right where it counts—your bottom line. It’s about taking the daily operational chaos and turning it into a process you can control, predict, and profit from.
The first thing you’ll notice is a huge leap in efficiency. Just think about all the time your team currently spends on manual data entry, hunting for misplaced paperwork, or trying to make sense of conflicting spreadsheets. An ERP handles those repetitive jobs automatically, letting your talented people focus on what really matters, like improving quality or innovating your next product. This isn’t just a minor improvement; it fundamentally changes how your business runs.
This efficiency boost flows directly into your production scheduling. The ERP links everything together in real time—sales orders, inventory levels, and machine availability—to get your workflows running smoothly. It helps you slash expensive downtime by spotting potential bottlenecks before they bring everything to a grinding halt, giving you a far more consistent output from the shop floor.
Gaining a Clear View of Everything
For many manufacturers, the biggest headache is not having a clear line of sight across the entire supply chain. A good manufacturing ERP is like a central nervous system for your business, letting you see everything with total clarity, from raw materials on order to finished goods sitting in the warehouse. This isn’t just a nice-to-have; it’s a massive strategic advantage.
With live data at your fingertips, you can stop reacting to inventory problems and start getting ahead of them. Instead of an operator discovering you’re out of a crucial part, the system flags it when stock levels get low. This foresight helps you avoid production stoppages and last-minute emergency shipping costs, ensuring you have what you need, exactly when you need it.
This newfound clarity also puts you in a much stronger position when dealing with suppliers. When you have detailed data on your purchase history, demand forecasts, and how well each supplier performs, you can negotiate from a place of confidence. Good data empowers you to lock in better pricing and more favourable terms.
An ERP transforms your data from a scattered collection of records into a powerful decision-making engine. It provides the single source of truth needed to cut waste, improve quality control, and drive profitability across every department.
Making Smarter Decisions with Centralised Data
Bringing all your operational data into one place does more than just tidy up your digital files; it powers better, faster decision-making. With real-time dashboards and analytics, managers can see how things are going at a glance, spot emerging trends, and tackle issues before they escalate.
Think about what this looks like in practice:
- Improved Quality Control: You can trace materials from the moment they arrive to final shipment. This makes it so much easier to pinpoint the source of any defects and maintain consistently high standards.
- Simplified Compliance: Need to generate a detailed report for a regulatory body? It’s just a few clicks away. This takes the stress out of audits and makes sure you’re always meeting industry requirements.
- Accurate Costing: Finally understand the true cost of every single product. The system precisely tracks labour, materials, and overheads, which leads to much smarter and more profitable pricing strategies.
This shift towards data-driven operations is picking up serious speed. The Australian Enterprise Resource Planning (ERP) market is on a strong growth trajectory, with forecasts predicting it could hit AUD 10.37 billion by 2034. This growth highlights a nationwide move towards digital automation in manufacturing, all driven by the need for real-time information and tighter operational control. You can discover more about the Australian ERP market growth and its drivers.
Building Your Perfect ERP with Core Modules
Off-the-shelf software just doesn’t cut it for most manufacturers. Your operation is a complex machine with its own unique quirks and demands, and your ERP needs to be built to match. It’s best to think of an ERP not as a single program, but as a customisable toolkit. Each tool, or module, is designed to handle a critical part of your business.
The real power comes from picking the right combination of these modules to solve your specific challenges. It’s like building the perfect engine for a high-performance car; every component has to work flawlessly with the others to drive the whole operation forward. When you select the right modules, you create a central system that truly speaks the language of your shop floor.
This image shows how a fully integrated ERP, built from these essential modules, can support a modern assembly line by connecting different operational functions.
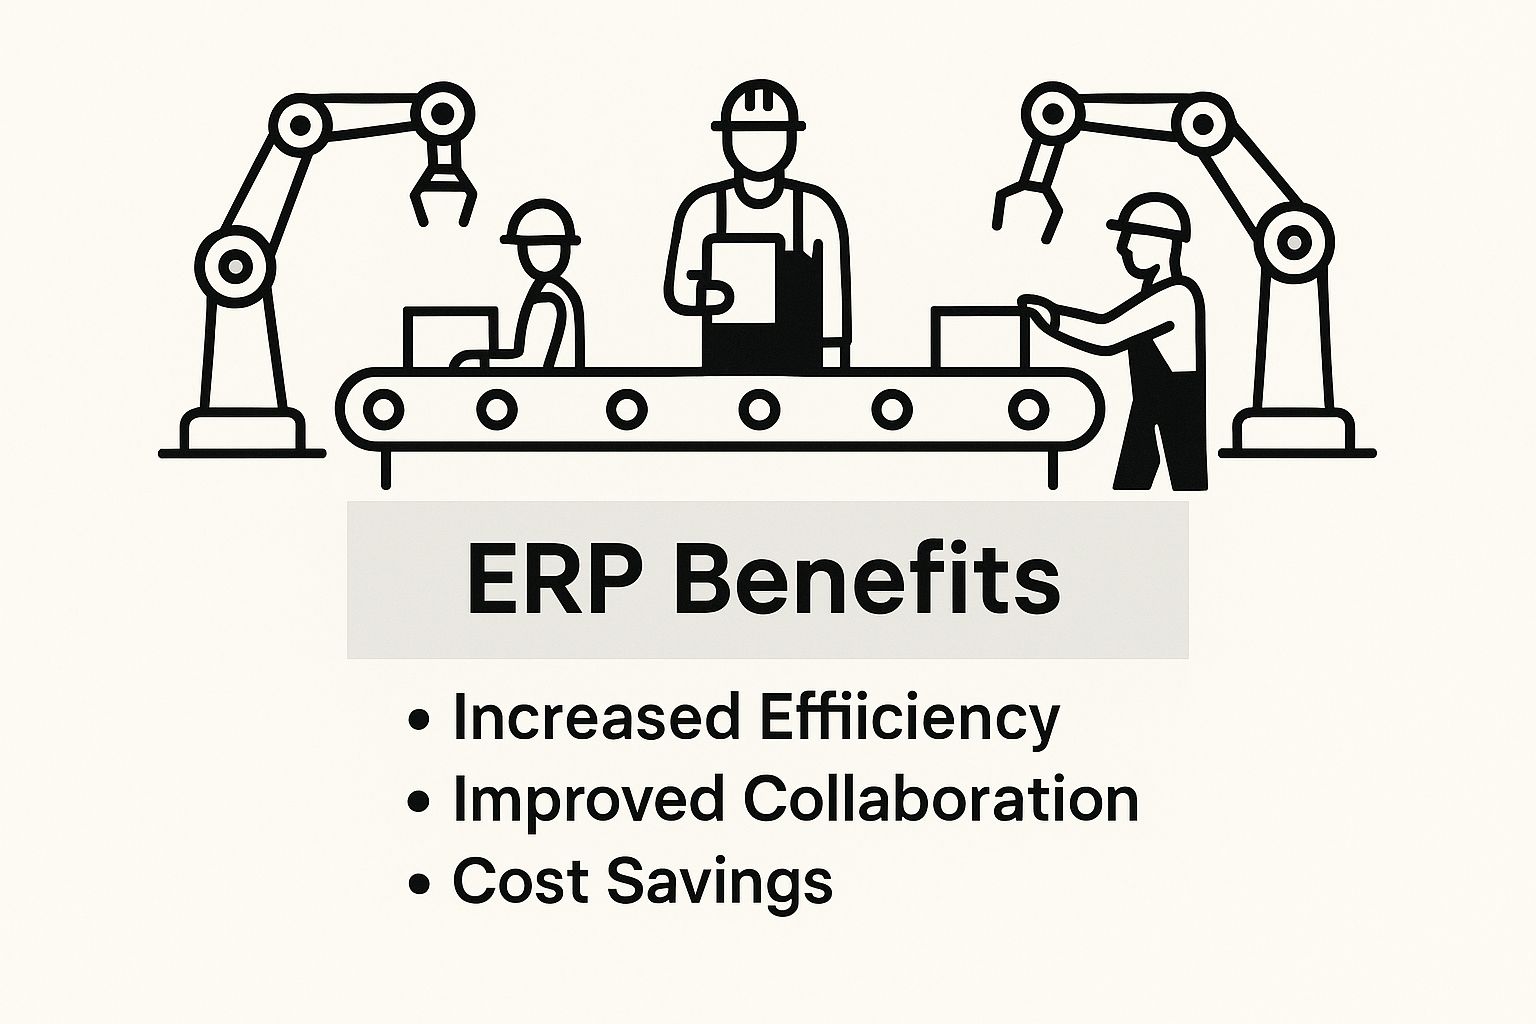
As the graphic illustrates, an ERP’s strength lies in its ability to bring everything together—from robotics to human labour—under one cohesive digital roof.
Production and Shop Floor Management
At the very heart of any manufacturing ERP is the production management module. This is your command centre for the entire manufacturing lifecycle. It takes you from planning and scheduling jobs right through to tracking their progress on the shop floor in real time.
This module helps you map out detailed production plans based on sales orders and demand forecasts. From there, it generates work orders and sends them to the right workstations, ensuring work flows smoothly and logically. For managers, it’s a live dashboard view of everything that’s happening, flagging potential bottlenecks before they cause major delays.
A strong production module transforms your shop floor from a reactive environment into a proactive one. It gives you the control to optimise machine usage, manage labour effectively, and ensure every job stays on schedule and within budget.
Ultimately, this module is all about answering critical questions like, “Do we have the capacity to take on this new order?” and “What’s the current status of Job #1138?”
Inventory and Materials Management
Good inventory management is a tough balancing act. Hold too much stock, and you’re tying up valuable capital. Hold too little, and you risk a costly production shutdown. The inventory management module gives you the data-driven precision needed to get this balance just right.
It keeps tabs on every single component, from raw materials to finished goods, across all your warehouses and locations. The system can even automate reorder points, so you never run out of critical parts unexpectedly. It also provides tools for demand forecasting, helping you anticipate what you’ll need based on past sales data and market trends.
This functionality directly prevents two of manufacturing’s most expensive problems:
- Stockouts: By maintaining optimal inventory levels, you make sure the production line always has the materials it needs to keep running.
- Overstocking: You avoid wasting money on excess inventory that just sits in the warehouse, gathering dust and potentially becoming obsolete.
Supply Chain Management and Quality Control
Your manufacturing process doesn’t begin or end at your factory doors. The Supply Chain Management (SCM) module expands your view outward, helping you manage supplier relationships, logistics, and procurement with far greater efficiency. It lets you track supplier performance, manage purchase orders, and monitor shipments to get ahead of potential disruptions.
Working hand-in-glove with SCM is the Quality Management module. This component is all about upholding your product standards at every single stage. It allows you to define quality control parameters, schedule inspections, and track any non-conformance issues. If a batch of raw materials from a supplier fails an inspection, the system can automatically flag it, stopping defective components from ever hitting the production line. This integration is vital for protecting your brand’s reputation and cutting down the cost of rework or recalls.
The table below breaks down how these core modules tackle specific, everyday challenges on the factory floor, showing their direct impact on your operations.
Essential ERP Modules and Their Manufacturing Functions
| Module Name | Primary Function | Problem Solved in Manufacturing |
|---|---|---|
| Production Management | Plans, schedules, and tracks all work orders and shop floor activities. | Prevents production bottlenecks and provides real-time job status. |
| Inventory Management | Monitors stock levels, automates reordering, and forecasts material needs. | Eliminates costly stockouts and reduces excess inventory holding costs. |
| Supply Chain Management | Manages supplier relationships, procurement, and logistics. | Improves supplier reliability and provides visibility into incoming shipments. |
| Quality Management | Defines and enforces quality standards, tracks inspections, and manages defects. | Reduces rework and ensures every product meets customer expectations. |
| Financial Management | Integrates production costs with the general ledger for accurate accounting. | Provides a true understanding of product profitability and overall financial health. |
As you can see, each module plays a distinct but connected role. Together, they create a comprehensive system that gives you complete control over your manufacturing environment.
How to Choose the Right ERP Solution
Picking from the massive list of ERP solutions for manufacturing can feel completely overwhelming. With so much riding on the decision, getting it wrong can lead to years of friction on the shop floor and a huge amount of wasted cash. The trick is to approach this with a clear, methodical plan that’s all about your business—not just the flashy features a salesperson is pushing.
Think of it like buying a new truck for your delivery fleet. You wouldn’t just grab the one with the biggest engine. You’d be looking at its payload, fuel economy, and running costs to make sure it’s the right tool for the job. Your ERP is no different; it has to fit your unique operational needs like a glove.
This means you need to look past the sales pitch and really dig into how a system will work day-to-day, and, just as importantly, how it will grow with you. Let’s break down the essential factors you need to get right.
Selecting Your Deployment Model
One of the first big forks in the road is deciding where your ERP system will actually live. Your choice between on-premise, cloud, or a hybrid setup will have major knock-on effects for your budget, how your team accesses it, and the load on your IT crew.
-
On-Premise ERP: This is the old-school way. You buy the software licences outright and run the whole show on your own servers, in your own building. This gives you total control, but it also means a massive upfront cost for hardware and the need for an in-house IT team to keep it all running smoothly.
-
Cloud-Based ERP (SaaS): With this model, you’re essentially renting the software. You pay a subscription fee to a provider who hosts and manages everything for you. This dramatically lowers the initial investment, makes updates a breeze, and lets your team log in from anywhere—a game-changer for businesses with multiple sites or remote staff.
-
Hybrid ERP: This is a mix-and-match approach. You might keep super-sensitive financial data on your own servers but use cloud apps for things like CRM or supply chain management. It offers a nice balance of control and modern flexibility, but can make your IT setup a bit more complex.
For Australian manufacturers, especially those in mining or agriculture with operations spread across vast distances, cloud-based systems are fast becoming the default. The ability to access real-time data from a remote site office is invaluable. You can explore more about ERP trends in Australia to see how local businesses are using the cloud to stay agile.
Evaluating Scalability and Vendor Support
Your business isn’t going to stand still, and your ERP can’t afford to either. A system that’s a perfect fit today could become a frustrating bottleneck in five years. This is why scalability is absolutely non-negotiable.
When you’re talking to potential vendors, hit them with the tough questions. Can the system cope if our transaction volume doubles next year? How painful is it to add new users, new production lines, or even a whole new factory? The right ERP should feel like a partner in your growth, not something holding you back.
An ERP is a long-term partnership, not a one-time purchase. The quality of vendor support is just as important as the software itself. A great system with poor support can quickly become a source of frustration.
Never underestimate the importance of the vendor relationship. Before you even think about signing a contract, do a deep dive into their support structure. What are their guaranteed response times? Critically, do they offer local Australian support, so you’re not trying to get help from someone on the other side of the world? A responsive support team is your lifeline, both during the initial rollout and for years to come.
Understanding the Total Cost of Ownership
Finally, you have to look beyond the price on the quote and work out the Total Cost of Ownership (TCO). That initial number is almost always just the tip of the iceberg.
To get a true picture of the investment, you need to map out every single associated cost over the system’s entire lifespan. This gives you a realistic budget and saves you from some very nasty surprises down the track.
Make sure your TCO checklist covers these key areas:
- Software Licensing: The upfront purchase or the ongoing subscription fees.
- Implementation Costs: The bill for getting the system set up, configured, and for moving all your old data across.
- Hardware & Infrastructure: The cost of servers and network gear if you’re going with an on-premise system.
- Training Fees: The money you’ll need to spend to get your entire team comfortable and proficient with the new software.
- Ongoing Support & Maintenance: The annual fees for vendor support, updates, and patches.
By carefully working through each of these points, you can shift from feeling overwhelmed to being in control. This structured process ensures you choose an ERP solution for manufacturing that not only solves today’s problems but also lays a solid foundation for whatever comes next.
Your Roadmap for a Successful ERP Implementation
Choosing the right ERP is a massive step, but the real work has only just begun. Even the most powerful software will fall flat if the implementation is fumbled. A chaotic rollout quickly leads to frustrated staff, major disruptions to your operations, and a very expensive investment going down the drain. To get it right, you need a clear, well-thought-out roadmap.
Think of this roadmap as your guide, steering you through the critical phases of turning a piece of software into the central nervous system of your business. It’s far more than just installing a program; it’s about leading your people through a significant change and setting them up to win from day one. Done right, your new system will be embraced, not just tolerated.
Phase 1: Assembling Your Team and Plan
Your very first move? Secure executive buy-in. Your leadership team has to be the project’s biggest champion, allocating the necessary resources and authority to get it over the line. Without enthusiastic support from the top, the project is likely to stall the moment it hits the first bump in the road.
Next up, build your dedicated project team. This isn’t a job for someone to do in their spare time. Your team needs to include key people from across the business—operations, finance, IT, and especially the shop floor. This cross-functional approach ensures every department’s needs are considered and the final system actually works for the people who will use it every day.
A successful ERP implementation is 20% technology and 80% people and process. The focus must be on managing organisational change, not just installing a new IT system.
With your team in place, it’s time to create a detailed project plan. This document is your blueprint. It should spell out clear goals, a realistic timeline with key milestones, and a firm budget to keep everyone aligned and the project on track.
Phase 2: Data Migration and System Configuration
This is where many projects run into serious trouble: moving all your historical data from the old systems into the new ERP. The biggest pitfall here is “dirty data”. Migrating inaccurate or incomplete information is like pouring sludge into the tank of a brand-new car—it just won’t run properly.
You absolutely have to take the time to cleanse and validate your data before you even think about migrating it. This means hunting down and removing duplicates, correcting errors, and getting everything into a standard format. It’s a tedious process, no doubt, but it’s essential if you want the new system to provide reliable insights from the moment it goes live.
Once your data is clean, you can start configuring the system. This is all about tailoring the ERP modules to your specific manufacturing workflows. The goal is to make the system support how you work, not force you to change your processes to fit the software. This is where having a flexible ERP and a knowledgeable implementation partner really pays off.
Phase 3: Training and Go-Live Preparation
Poor training is one of the biggest reasons new systems fail to get adopted by staff. You must invest in comprehensive training sessions for every single person who will touch the new system. Critically, this training should be role-specific, showing each employee exactly how the ERP will make their day-to-day tasks easier, not harder.
Before the big day, run a “go-live” rehearsal or a pilot test in a practice environment. This lets a small group of users test the system with real-world scenarios, which is a fantastic way to catch and fix any last-minute bugs before the full launch. It also builds confidence and helps smooth out the final transition.
As you get ready, keep in mind that integrating a new ERP with your existing legacy machinery and infrastructure can be complex and slow things down. Looking ahead, AI-augmented ERP solutions are on the horizon, promising better predictive analytics—something vital for modern Australian manufacturing. You can find out more about the future of the Australian ERP market on nextmsc.com.
Finally, the go-live itself needs to be meticulously planned. It’s often best to schedule it during a quieter period, like over a weekend, to minimise business disruption. Make sure your vendor’s support team and your own IT crew are on standby to jump on any immediate problems. This preparation is key to a smooth and successful start.
Your Top Manufacturing ERP Questions, Answered
Thinking about a new ERP system for your manufacturing business? It’s a big decision, and it’s completely normal to have a long list of questions. After all, this is a major investment in both time and money, so getting clear, straight answers upfront is non-negotiable.
Let’s walk through some of the most common questions we hear from manufacturers. The goal here is to cut through the noise and give you the practical insights you need to make the right call.
How Long Does an ERP Implementation Take?
This is usually the first question on everyone’s mind, and for good reason. While there’s no magic number, a typical ERP project for a small to medium-sized manufacturer usually takes somewhere between six to twelve months.
Of course, that timeline can stretch or shrink. The biggest factors are the complexity of your business, how much customisation you need, and the number of modules you’re bringing on board. If you’re running a larger, multi-site operation, it’s not uncommon for an implementation to take 18 months or more. The heavy lifting usually happens during data migration, user training, and the final testing phase—that’s where you iron out all the kinks before the big go-live.
Generic ERP vs. Manufacturing ERP: What’s the Difference?
So, can’t you just use a standard, off-the-shelf ERP? You could, but you’d be missing the point. A generic system is built for general business tasks—think finance, HR, and basic sales. It does that stuff well, but it’s completely out of its depth when it comes to the factory floor.
A manufacturing ERP is a different beast altogether. It comes packed with modules designed specifically for the realities of production. We’re talking about tools like:
- Shop Floor Control: Giving you a live view of every job as it moves through production.
- Bill of Materials (BOM) Management: The detailed recipes for everything you build.
- Production Scheduling: Helping you get the most out of every machine and every team member.
- Material Requirements Planning (MRP): Making sure you have the right parts on hand, right when you need them.
Put simply, a manufacturing ERP is built from the ground up to handle the entire journey from raw materials to finished products. A generic system just wasn’t designed for that world.
Can an ERP Integrate with My Machinery?
Yes, and this is where things get really powerful. Modern ERP systems are designed to talk directly to your equipment on the shop floor. This is often done using Industrial Internet of Things (IIoT) sensors, which send a constant stream of real-time data from your machines straight into the ERP.
This connection gives you incredible transparency. Suddenly, you’re not guessing about machine uptime or output; you know for sure. Your ERP can also link up with other key software you rely on, like your CAD programs or warehouse management systems (WMS). The key is to have these integration conversations with potential vendors early on. You need to be certain their system can plug into your unique tech stack without a hitch.
At Wistec, we focus on building practical, solution-driven technology that makes business operations smoother. If you’re exploring an affordable, scalable, and fully customised Odoo ERP solution, we can help you design a system that delivers real results for your manufacturing business. Discover how we deliver solutions through technology at https://www.wistec.com.au.